Rotary Slitter Blades · Slitter Knives
Precision Slitter Knivesfor Metal, Paper, Film & Converting Lines
D2, HSS M2, HSS M35 and powder-metal blades, vacuum heat-treated to 60–66 HRC, CNC-ground to ±0.0015 mm thickness tolerance and 0.2 Ra surface finish. Custom manufactured to drawing or sample. Shipped to 88 countries.
- ±0.0015 mm thickness tolerance, 0.2 Ra lapped finish
- 4-week standard lead time, 2-week rush available
- In-house vacuum heat treatment — no sub-contracting
- Mill certs, hardness certs & inspection reports included
Circular Slitting Blades
Built for Precision Coil Cutting
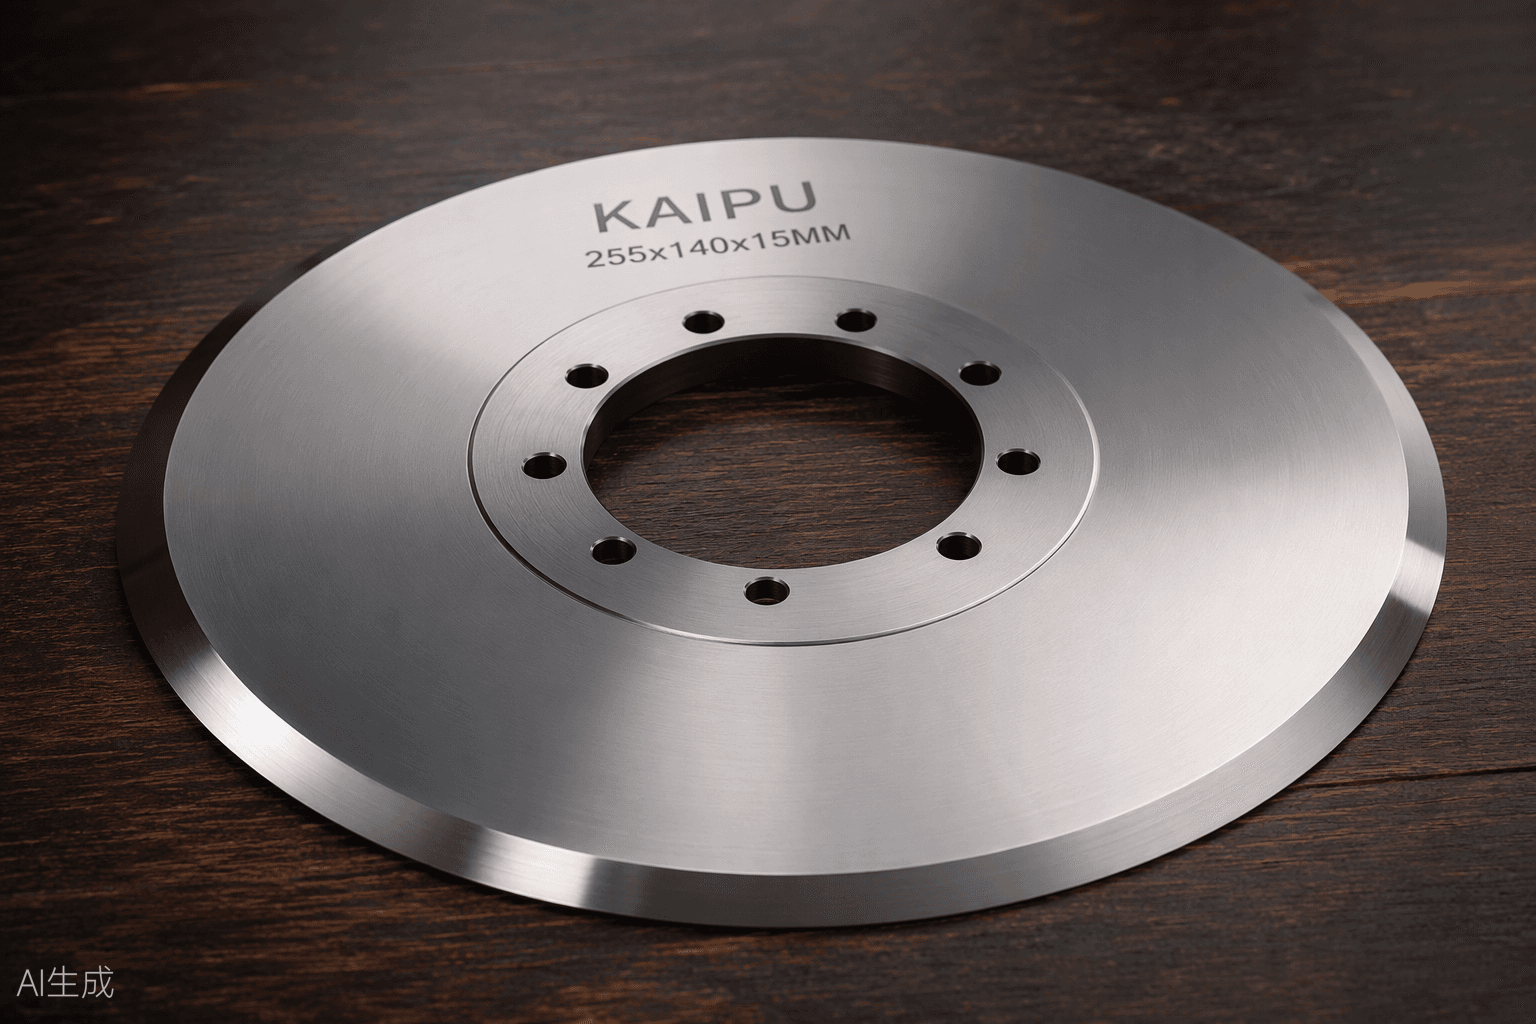
At KAIPU, we manufacture precision rotary slitter blades and slitter knives for coil cutting, sheet metal processing, and high-speed slitting lines across steel, aluminium, stainless, copper, and electrical steel applications.
Every blade is made in-house at our Ma'anshan facility — from raw material selection through vacuum heat treatment and CNC precision grinding, with no sub-contracting at any stage. Our in-house vacuum hardening furnace ensures uniform HRC across every blade cross-section, eliminating the soft-spot failures that cause premature chipping and burr on coil slitting lines.
- Zero runout: within 0.005 mm TIR on every blade
- Burr-free cutting: lapped to 0.2 Ra with matched edge geometry
- Extended tool life: 1.5× to 2.5× longer between regrinds vs. standard grades
- Custom in 4 weeks: to drawing, sample, or OEM part number
- Full documentation: mill certs, hardness certs, inspection reports included
Technical Specifications
No Guesswork. No Ambiguity.
Every specification below is verified per blade by our quality team before dispatch. Material test certificates and dimensional inspection reports are included with every shipment at no extra cost.
Material Selection Guide — Which Grade for Your Application
| Grade | HRC | Best Application | Max Strip Thk | Edge Life | Lead Time |
|---|---|---|---|---|---|
| D2 | 60–62 | HR/CR/GI coil slitting, general purpose | 6 mm | 1.0× (baseline) | 4 wks |
| HSS M2 | 62–64 | Stainless steel, silicon steel, high-speed lines | 4 mm | 1.5× | 4 wks |
| HSS M35 | 63–65 | Hardened SS & CRGO electrical steel | 3 mm | 1.8× | 5 wks |
| H11 / H13 | 50–55 | Hot rolled coil, side trimming | 12 mm | 0.8× at high temp | 4 wks |
| PM ASP2030 | 64–66 | Premium long-life critical applications | 4 mm | 2.5× | 6 wks |
Dimensional & Tolerance Specifications
| Outer Diameter Range | 75 mm to 600 mm (2.95 in to 23.62 in) |
| Inner Diameter Range | 20 mm to 250 mm (0.79 in to 9.84 in) |
| Thickness Range | 1.0 mm to 25 mm (0.04 in to 0.98 in) |
| Thickness Tolerance | ±0.0015 mm (±0.000059 inch) |
| Flatness Tolerance | ±0.001 mm (±0.000039 inch) |
| Parallelism | Within 0.005 mm TIR |
| Concentricity / Runout | Within 0.005 mm TIR |
| Surface Finish | Lapped to 0.2 Ra µm, polished to 0.1 Ra on request |
| Edge Geometry | Single bevel, double bevel, dished (concave/convex), radius edge |
| Cutting Capacity | 0.1 mm to 24 mm material thickness |
| Heat Treatment | In-house vacuum hardening & multi-stage tempering |
| Hardness Verification | 100% inspected per blade, portable hardness tester |
| CMM Inspection | CMM dimensional certificate per batch |
| Marking | Laser-etched part no., batch number & date on every blade |
How to Order
Specify Your Slitter Blade in 5 Steps
Material & Thickness
State material to be slit and thickness range (e.g. CR steel, 0.4–1.6 mm).
Strip Width & Tolerance
Specify required slit width and acceptable edge tolerance.
Arbor Dimensions
Provide existing arbor OD, ID, thickness, and keyway details if any.
Line Speed & Volume
Line speed in m/min and number of cuts per shift, if known.
Current Failure Mode
Current blade grade and what failure to eliminate: chipping, burr, edge wear, dishing.
Send a drawing, DXF, or used sample to sales@machine-knives.net. We respond within 1 working day with a grade recommendation, price, and delivery date.
Applications
Select Your Material & Configuration
Not all materials cut alike. Each card below is a real application KAIPU serves, with the recommended grade, hardness, and edge geometry drawn from production data — not a catalogue. Reference the configuration code when you contact us.
HR Coil Slitting — Mild & Structural Steel, 1.0–6.0 mm
- Grade
- D2 or H11
- Hardness
- 58–62 HRC
- Edge
- Single bevel 5–8°
- Typical
- 300 × 150 × 20 mm
Watch for edge wear at high gauge. Choose H11 for hot rolled where scale abrasion is severe.
Config Ref. KP-HR-01CR Coil Slitting — Low Carbon Steel, 0.3–3.0 mm
- Grade
- D2 or D3
- Hardness
- 60–62 HRC
- Edge
- Single bevel 6–8° + land
- Typical
- 255 × 140 × 15 mm
Burr is the primary failure mode on CR strip. Tight flatness tolerance is critical at thin gauges.
Config Ref. KP-CR-02GI / GA Coated Coil Slitting, 0.3–2.0 mm
- Grade
- D2 (TiN coated)
- Hardness
- 60–62 HRC
- Edge
- Radius edge or single bevel
- Typical
- 255 × 140 × 15 mm
Zinc coating causes accelerated blade wear. TiN surface treatment extends life 40–60%.
Config Ref. KP-GI-03Stainless Steel Coil — 200 / 300 / 400 Series
- Grade
- HSS M2 or M35
- Hardness
- 62–65 HRC
- Edge
- Single bevel 6° narrow land
- Typical
- 255 × 140 × 20 mm
Work-hardening material. Narrow land and high HRC prevent edge rollover.
Config Ref. KP-SS-04Aluminium & Aluminium Alloy Coil Slitting
- Grade
- D2 or HSS M2
- Hardness
- 58–62 HRC
- Edge
- Dished (concave) top blade
- Typical
- 280 × 160 × 18 mm
Soft material. Blade geometry drives edge quality more than hardness here.
Config Ref. KP-AL-05Silicon Steel / CRGO Electrical Steel Slitting
- Grade
- HSS M35 or PM ASP2030
- Hardness
- 63–66 HRC
- Edge
- Single bevel 5–7° narrow land
- Typical
- 255 × 140 × 15 mm
Extremely abrasive. Powder metal gives 2×–3× life vs standard HSS. Mandatory for CRGO.
Config Ref. KP-CRGO-06Copper & Brass Strip Slitting
- Grade
- D2 or D3
- Hardness
- 60–62 HRC
- Edge
- Double bevel or radius edge
- Typical
- 200 × 100 × 12 mm
Ductile metals can smear. Sharp geometry and correct lateral clearance are essential.
Config Ref. KP-CU-07Tube Mill Side Trimming
- Grade
- D2 or HSS M2
- Hardness
- 60–64 HRC
- Edge
- Square edge / side trim
- Typical
- 300 × 180 × 20 mm
Continuous contact demands maximum wear resistance. Pair with matched hardened spacers.
Config Ref. KP-TM-08Cut-to-Length Line Shear Blades
- Grade
- D2 or H13
- Hardness
- 58–62 HRC
- Edge
- Straight edge / shear angle
- Typical
- Custom to OEM spec
Shear angle and blade gap are critical. Always supply matched upper and lower blade sets.
Config Ref. KP-CTL-09Our Manufacturing Process
From Blank to Blade
Every KAIPU slitter blade passes through 6 tightly controlled in-house manufacturing stages. No sub-contracting at any step — CNC turning, CNC bore grinding, wire EDM for keyways, in-house vacuum hardening, and CMM quality verification.
Raw Material Cut
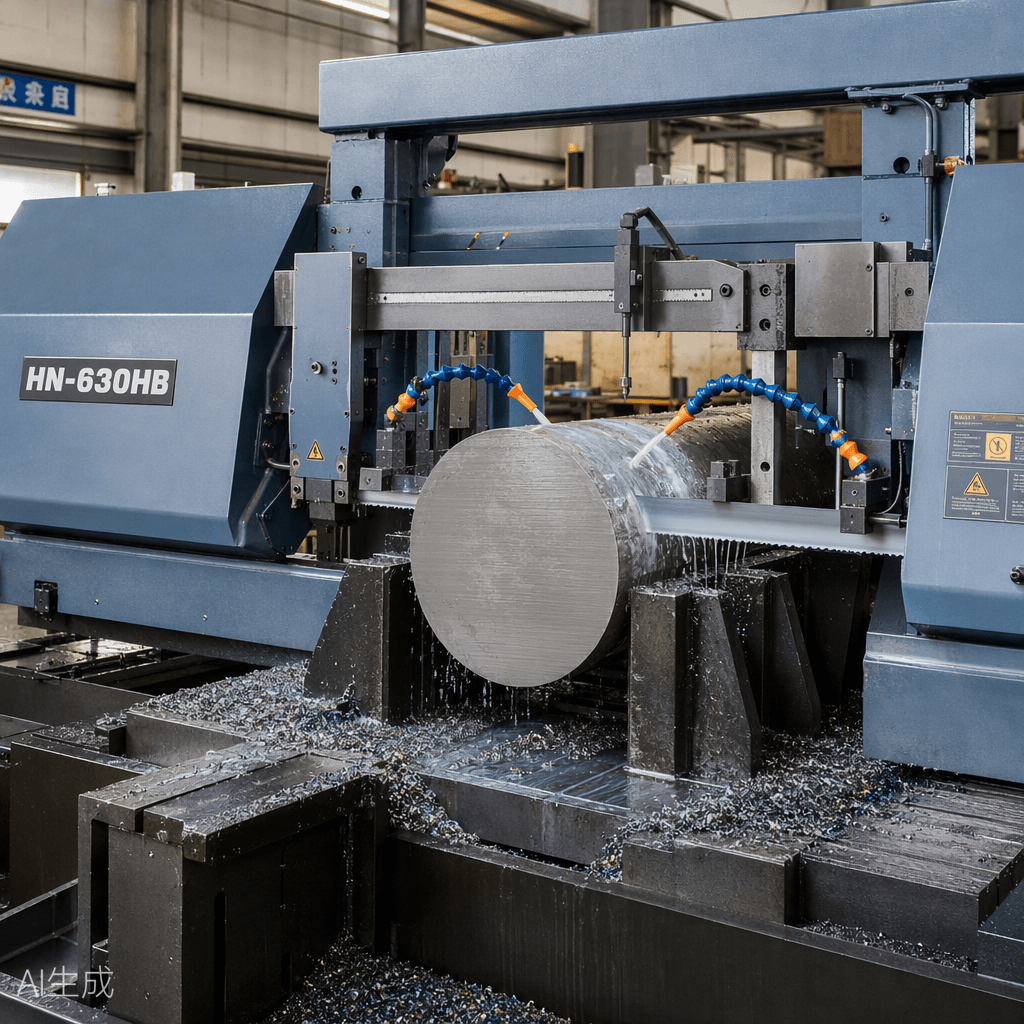
Bandsaw cuts certified D2/HSS billets. Mill certs retained per heat number.
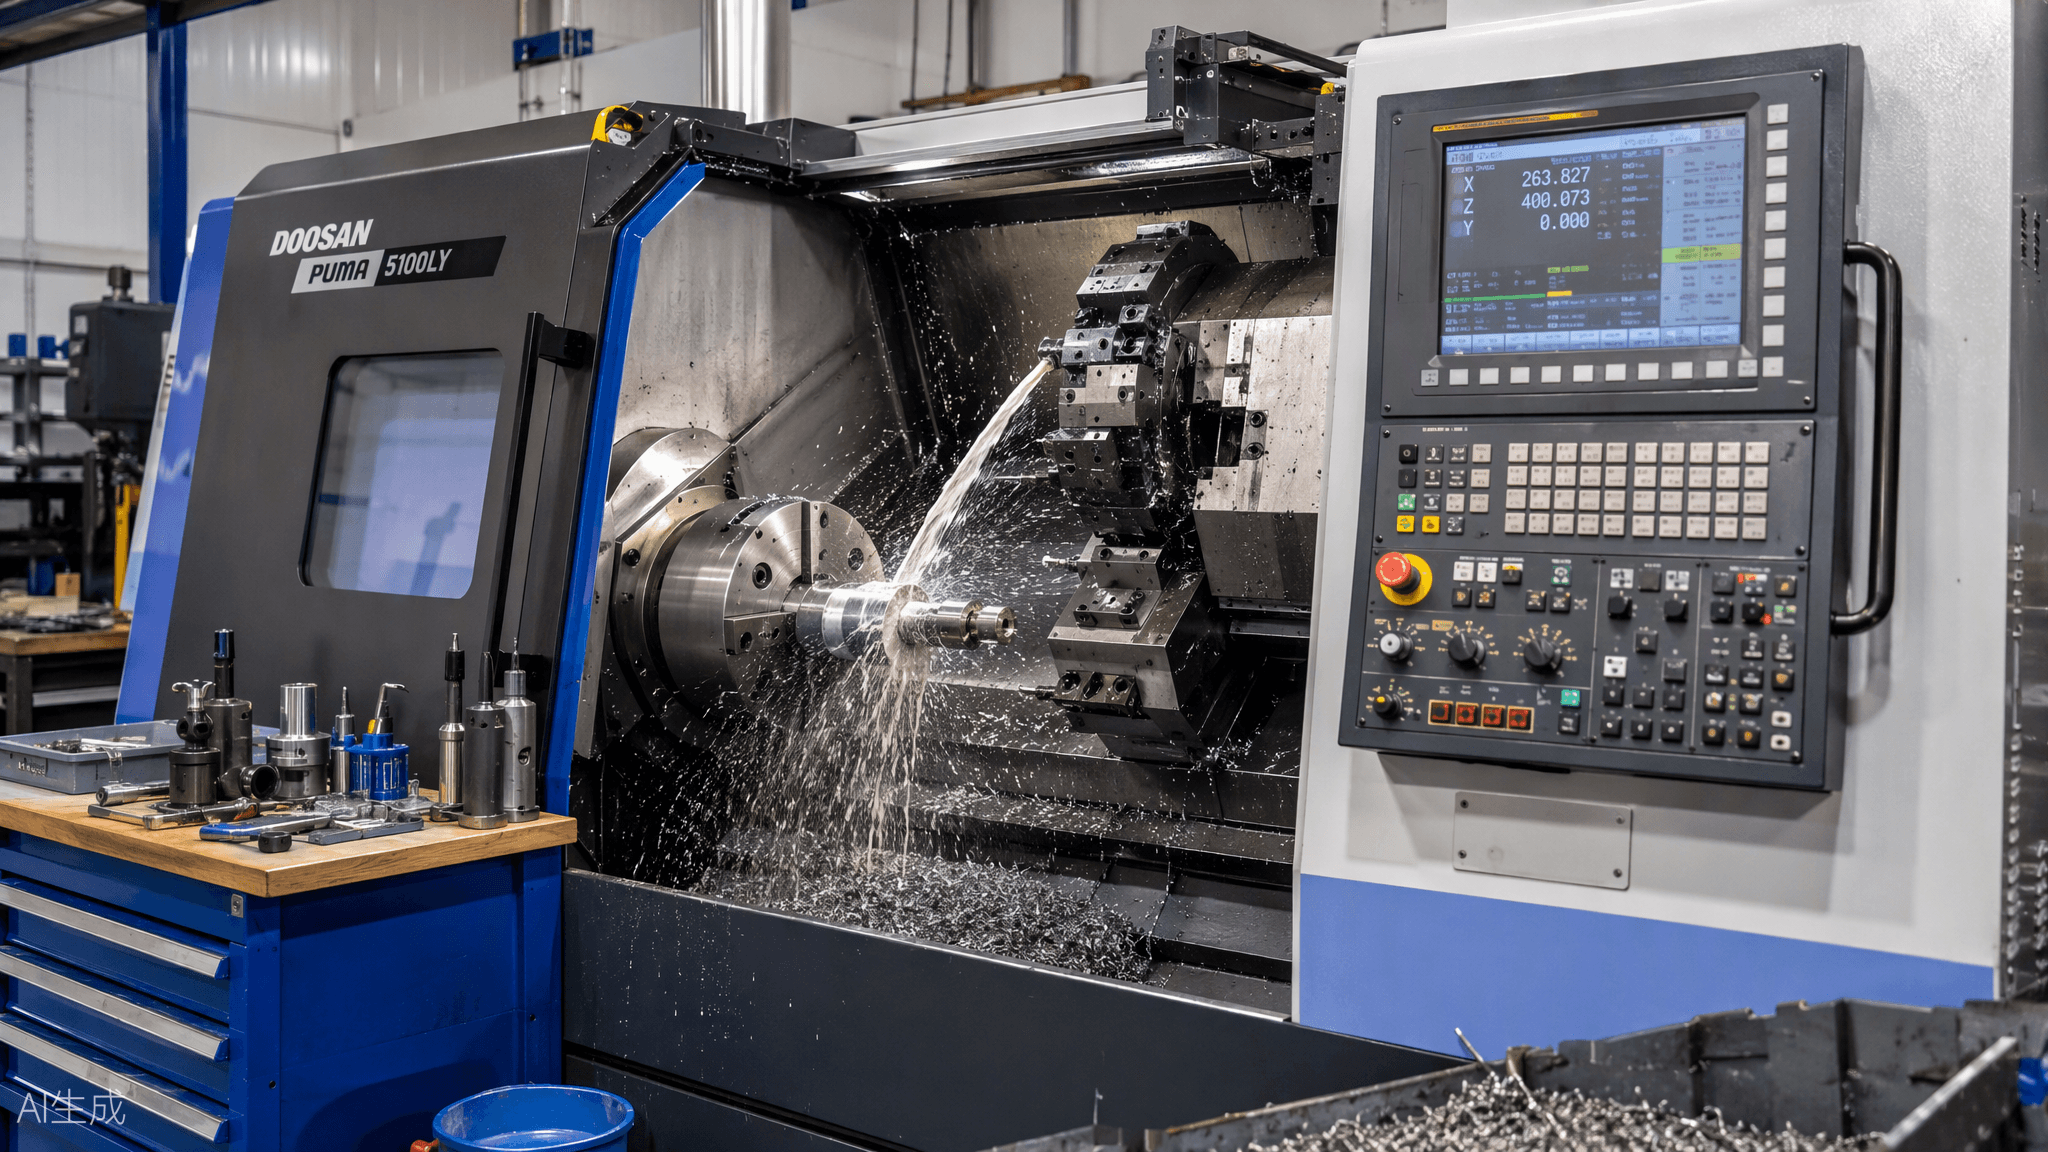
CNC Turning
CNC lathe faces & turns blanks to near-net OD, ID & thickness.
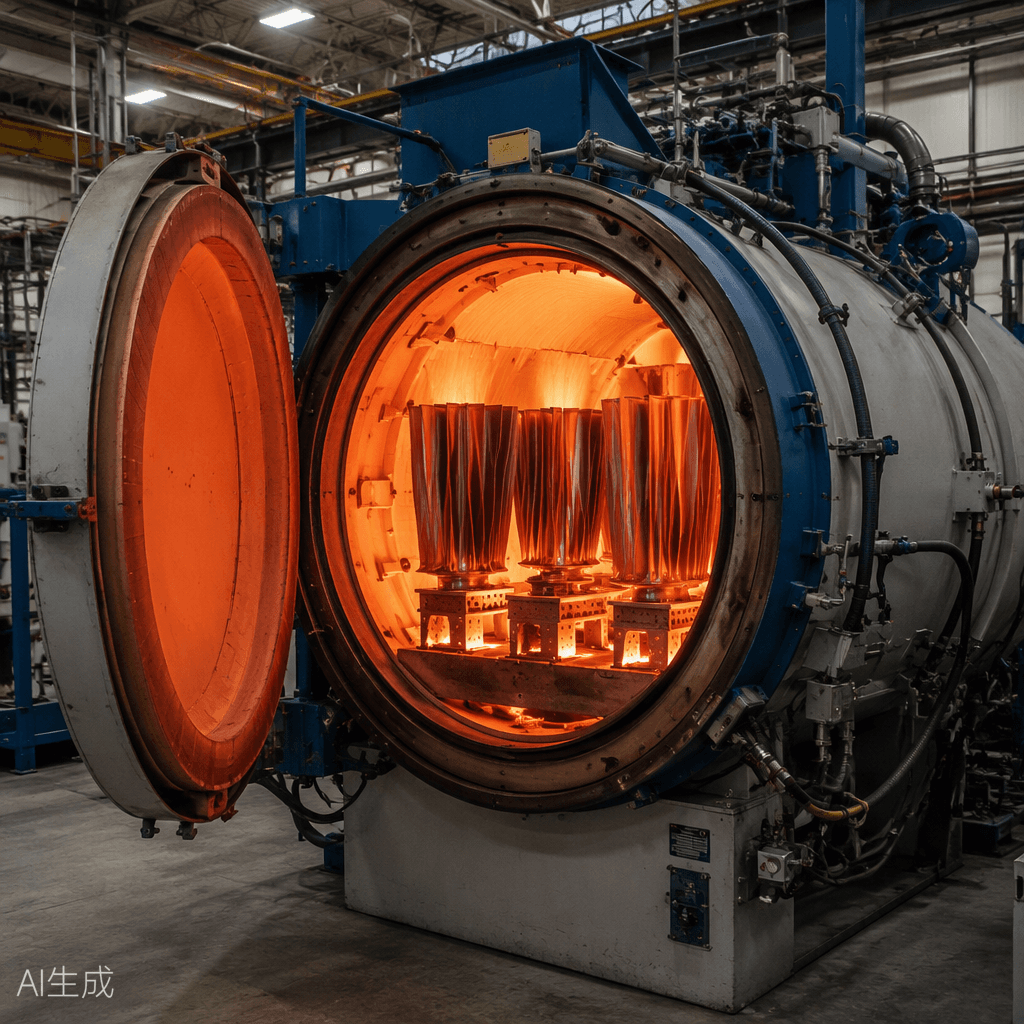
Vacuum Hardening
In-house vacuum furnace, multi-stage hardening & tempering to specified HRC.
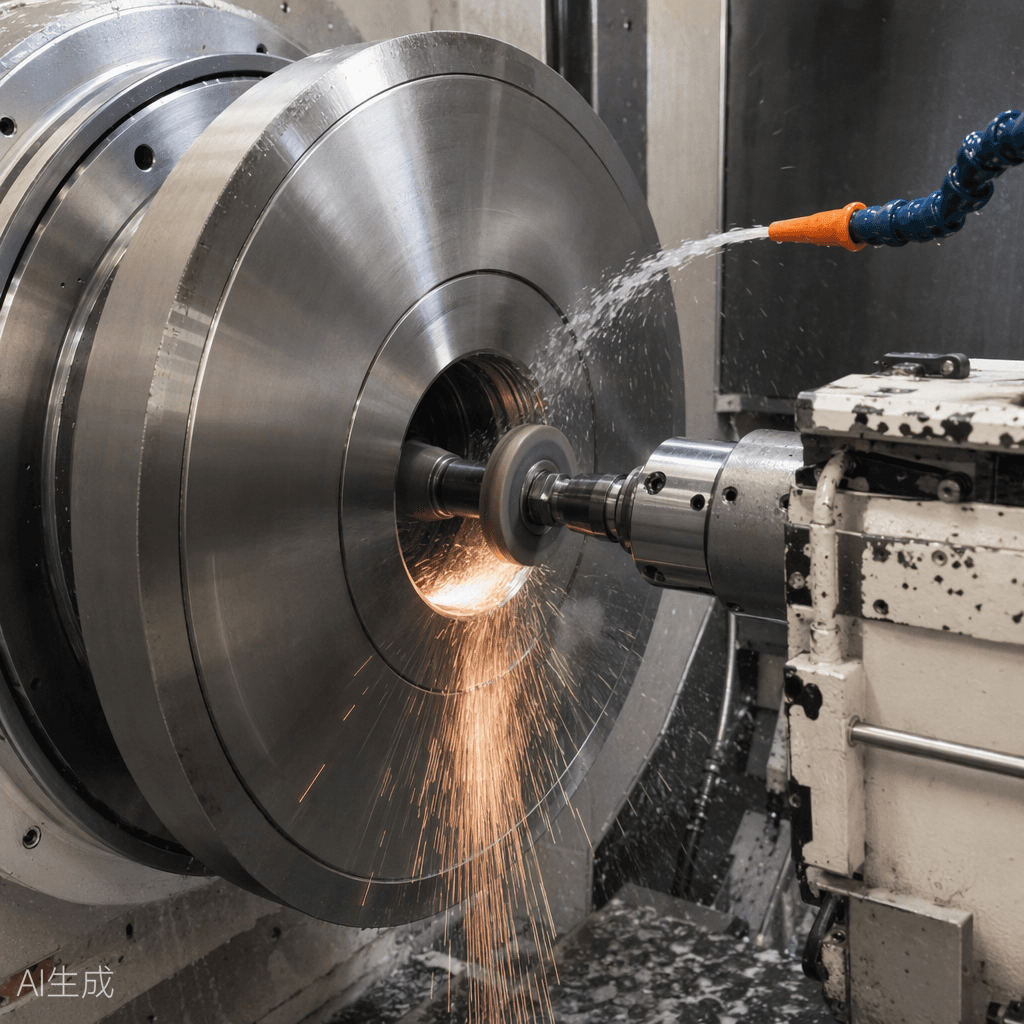
Bore Grinding
CNC internal grinder. Bore ground to final ID tolerance ±0.0015 mm.
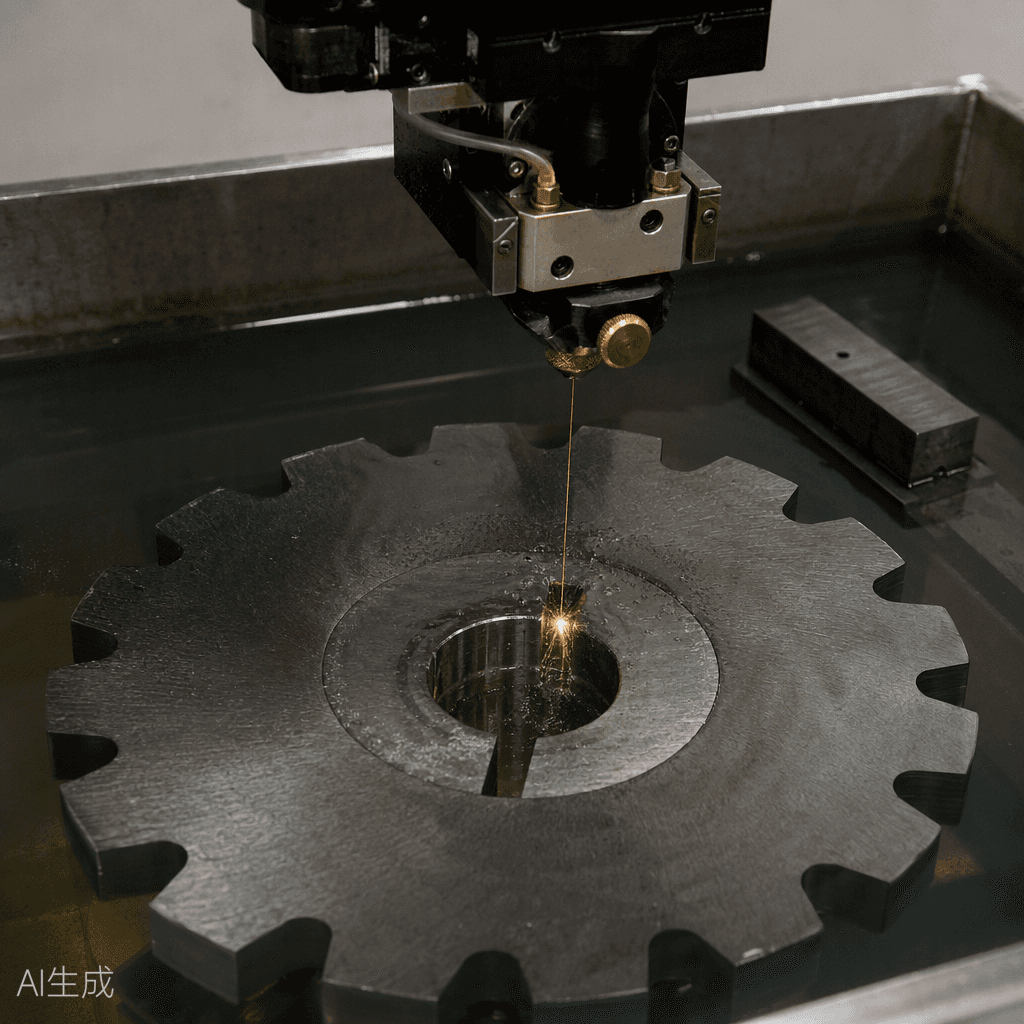
Keyway Wire EDM
Wire EDM machines keyways to precise width & depth, no distortion.
Laser Marking
Part no., dimensions & batch date laser-etched on every blade.
Inside Our Ma'anshan Manufacturing Facility
Real Machines. Real Blades.
Photographs of our shop floor. No CGI, no stock images. Each step shown is the actual machinery, in operation, producing the same blade you order.
Raw Material Cutting
Bandsaw cutting, D2 / HSS billets
CNC Turning
Precision CNC lathe
Vacuum Hardening
In-house vacuum furnace, to 66 HRC
Bore Grinding
CNC internal grinder
Keyway Wire EDM
Precision keyway cutting, no distortion
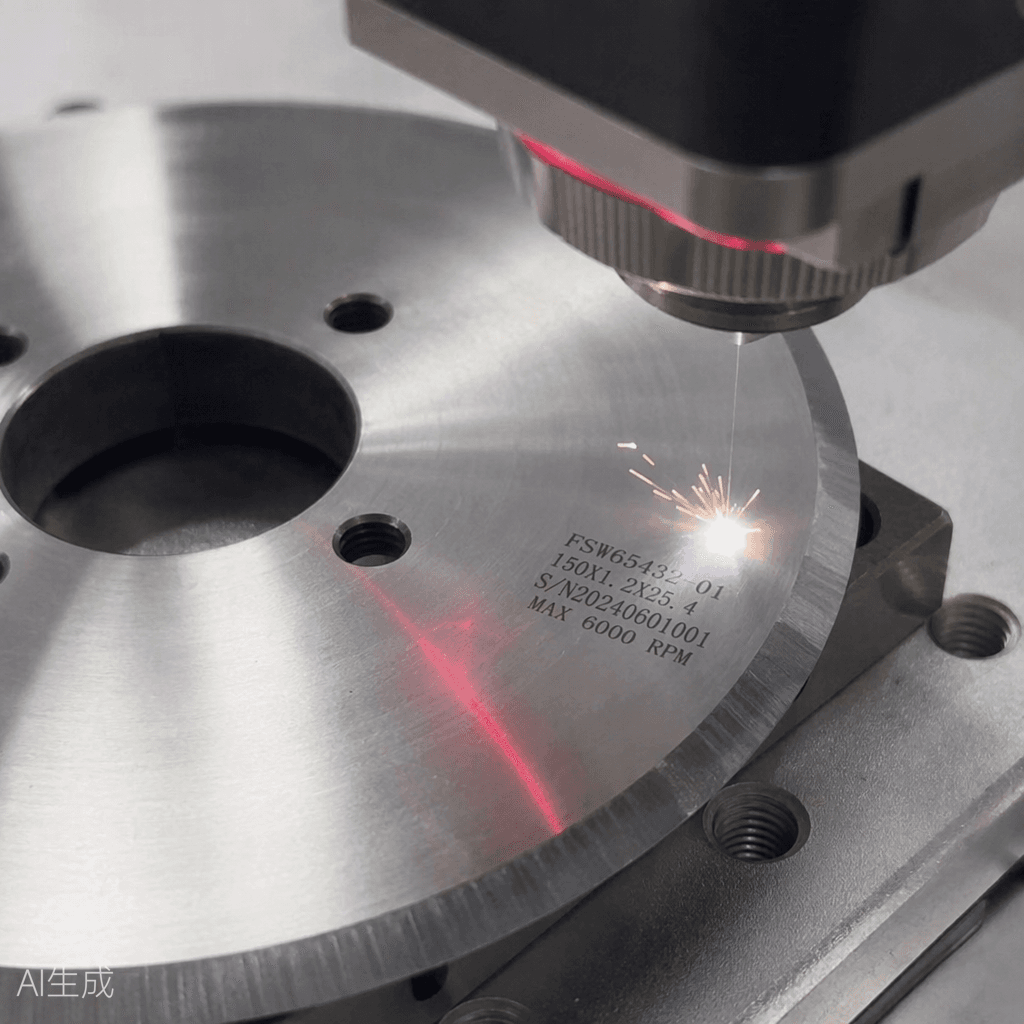
Laser Marking
Part No. + batch etched on every blade
Quality Control
Every Blade Inspected. Every Certificate Documented.
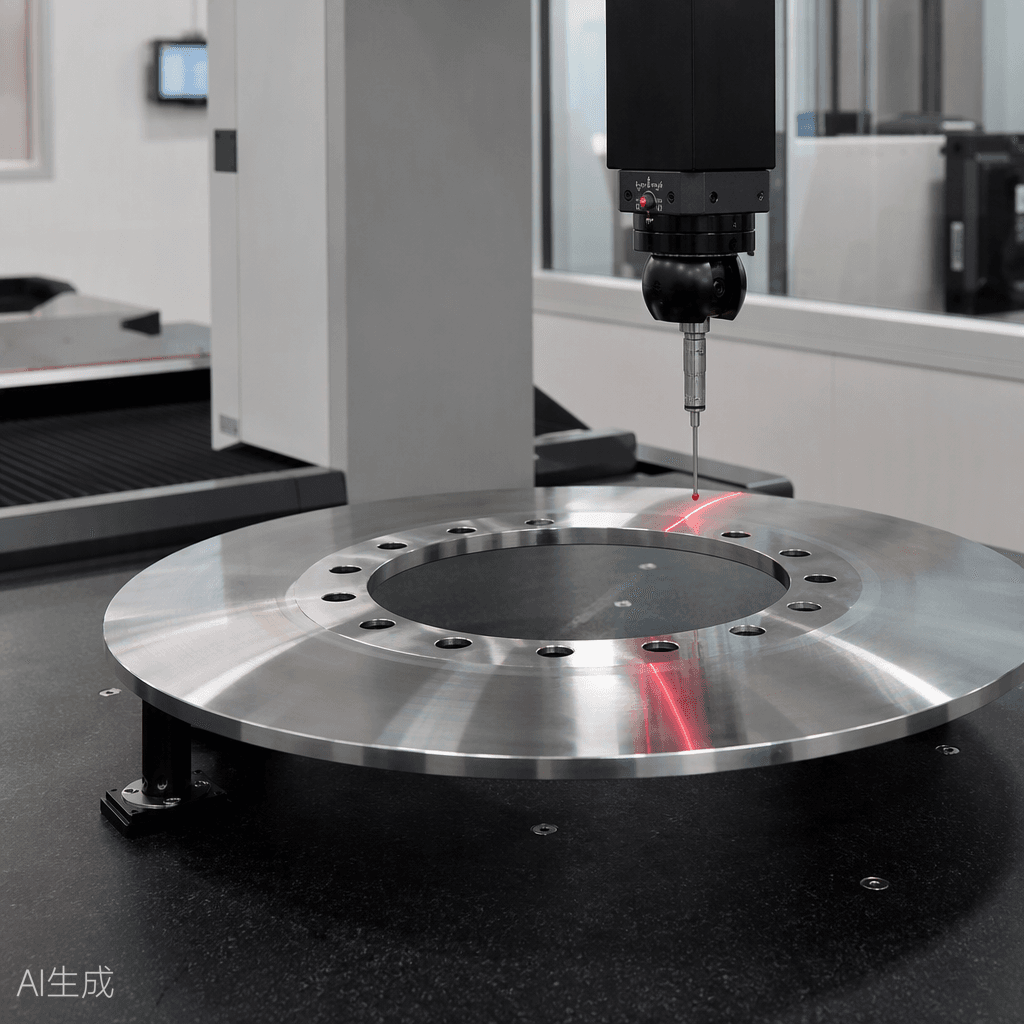
CMM (Coordinate Measuring Machine)
Our CMM performs 100% dimensional verification on every blade: OD, ID, thickness, parallelism, concentricity and runout, against your drawing tolerance.
Full inspection suite includes:
- CMM: OD, ID, thickness, runout per blade
- Portable hardness tester: HRC confirmed per blade
- Digital micrometers: thickness and flatness
- Surface roughness tester: Ra 0.2 µm confirmed post lapping
- Granite surface plate: flatness to ±0.001 mm verified
Material test certificates and CMM inspection reports are supplied with every shipment at no additional cost.
Case Studies
Real Results From Real Slitting Lines
Three case studies from KAIPU customers, with the actual problem, the blade change we recommended, and the quantified result. No "improved performance" vagueness.
SS Coil Service Center, UAE
HSS blades wore out every 6 to 7 days on 304 SS coil. Burr rejection rate: 3.1%. Customer was using local D2 blades.
Switched to KAIPU HSS M35, 64 HRC, single bevel 6° narrow land. Matched top + bottom set.
Blade life: 6 days to 17 days (+183%). Burr rejection: 3.1% to 0.3%. Monthly tooling cost down 34%.
Hot Rolling Mill, India
Side trimmer blades chipping within 4 days on 6 mm HR coil. Blade change downtime: 2.5 hrs per event.
Specified H11 at 52 HRC, radius edge, OD 350 × ID 200 × 25 mm. Supplied matched top/bottom sets + hardened spacers.
Blade life: 4 days to 11 days. Chipping: zero in 6-month review. Annual saving: ≈ $21,000 in tooling + downtime.
Aluminium Converter, India
Top dish blades dishing on 0.8 mm aluminium after 5 days. Edge quality inconsistent across slit widths.
Converted to D3 at 62 HRC, concave dished geometry, flatness 100% verified ±0.001 mm per CMM.
Top blade dish profile re-specified to match line tension. Edge quality consistent across all slit widths after changeover.
Regrinding Service
Regrinding Service, Extend Blade Life by 3 to 5 Cycles
Send your worn KAIPU or non-KAIPU blades to Ma'anshan. We regrind, re-lap, re-inspect and ship back to original dimensional tolerance, extending blade life by typically 3 to 5 regrinds on thin knives running heavy gauge, 30 or more on heavy tooling at a fraction of new blade cost.
Every regrind includes:
- Dimensional regrinding to original OD, ID and thickness
- Edge re-honing to original bevel angle and land width
- Lapping to 0.2 Ra surface finish, CMM dimensional verification per blade
- Hardness re-verification (portable hardness tester)
- Full inspection report shipped with return delivery
Turnaround: 10 working days from receipt of blades
Request Regrinding PickupGlobal Delivery
Shipped to 88 Countries. Quoted in Your Currency.
From a single replacement blade to a full line tooling set, we handle export packing, documentation and freight — door to door if you prefer.
Shipping Options
- DHL / FedEx express: 3–5 days
- Air freight: 5–8 days
- Sea freight (LCL/FCL): 20–35 days
- Rush dispatch on regrind return
Incoterms
- EXW Ma'anshan
- FOB Shanghai / Ningbo
- CIF / CFR major ports
- DDP door-to-door available
Currency & Payment
- Quoted in USD, EUR, GBP or your currency
- T/T bank transfer (30/70 or 100%)
- PayPal for samples & small orders
- L/C accepted for large orders
Export Packing & Docs
- VCI anti-rust paper + foam + plywood case
- Mill & hardness certs per batch
- Packing list, invoice, C/O on request
- Full dimensional inspection report
Frequently Asked Questions
Before You Ask
What are slitter blades and knives?
Slitter blades and knives are specialized cutting tools used in slitting machines to precisely cut large rolls of material into narrower strips.
What is a slitter blade used for?
Slitter blades are commonly used in industries like paper, plastic film, metal, textiles, and packaging, these blades ensure clean, accurate cuts with minimal material waste.
What material is used for manufacturing slitting blades?
Slitting blades are typically manufactured from high-performance materials such as D2 and D3 cold work tool steel, HSS M2 and M35, and PM-HSS ASP 2030, selected by strip material, gauge and line speed.
Can I order custom-sized slitter blades?
Yes, absolutely! At KAIPU Machine Knives, we specialize in manufacturing custom-sized slitter blades of different shapes and sizes including: rotary, circular and straight machine knives.
What types of materials can rotary slitter blades and knives handle?
They can handle various metals including steel, stainless steel, aluminium, copper, and other industrial alloys.
Are slitter blades and slitter knives the same?
Slitter blades and slitter knives are often used interchangeably, but slitter blades usually mean rotary circular cutters, while slitter knives may include different industrial cutting tools used in slitting, trimming, and converting machines.
What materials can slitter blades and slitter knives cut?
Slitter blades and slitter knives are designed to cut a wide range of materials depending on their material grade and hardness. They are commonly used for slitting materials such as metal sheets, paper, plastic films, foil, rubber, and laminates in industrial slitting and converting machines.
What is the hardness of slitter blades?
Slitter blades are usually hardened to about 58 to 60 depending on the tool steel used. Proper heat treatment provides wear resistance, longer blade life, and consistent cutting performance in high-speed slitting operations.
What should be checked before installing slitter blades?
Before installing slitter blades, check size, tolerance, flatness, alignment, and mounting surface condition. Ensure blades are clean, undamaged, and properly aligned with the shaft to prevent vibration, poor cutting, and machine wear.
Why use custom slitter blades instead of standard blades?
Custom slitter blades offer better fit, tighter tolerance, and longer life because they are made for specific machines and materials. This improves cutting accuracy, reduces burrs, and ensures stable performance in high-speed slitting operations.